Custom MOCVD Susceptor Design Boosts Epitaxy Uniformity and Yield
2026-10-10
Epitaxy engineers know the pain: a susceptor that works beautifully for one process can quietly sabotage the next, showing up as subtle thickness drift or doping non-uniformity. Off-the-shelf designs simply can’t account for every reactor geometry or thermal budget. That’s where custom susceptor engineering pays off. At Semicorex, we focus on tailoring every pocket, recess, and coating to the way you actually run MOCVD. The result? Tighter uniformity and a yield curve that finally stops dipping. Here’s what sets a well-designed custom susceptor apart—and why it may be the fastest route to better epi performance.
Where Standard Pocket Designs Lose Thermal Uniformity
Sewn-through pocket construction is usually the first point of failure. At every stitch line, the insulation gets crushed to a fraction of its intended loft, and the two shell fabrics meet almost directly. Those narrow compressed channels act like thermal wicks, pulling heat out along the entire seam grid. You can see it on a thermal camera: a faint but consistent web of cold lines running across the jacket, even when the fill power is high. The result is an overall thermal resistance that sits well below what the material spec suggests, with cold seams that are impossible to feel in a showroom but obvious outside.
A less visible issue comes from pocket sizing and fill migration. When standard pockets are cut a little too generously for the amount of down they hold, the insulation shifts under gravity and repeated movement. The upper sections of each pocket lose density, while the lower corners become overstuffed and stiff. This creates a vertical gradient in warmth, with cold patches appearing near the shoulders and around the waist where the fabric is left nearly uninsulated. Because the shell hides the migration, the wearer often discovers the unevenness only after an hour or two in real cold.
Box-wall and differential-cut pockets solve some of this, but introduce their own kind of thermal nonuniformity. Rigid internal dividers create discrete air chambers that can pump warm air out during motion. Every time the fabric flexes, one pocket compresses while the adjacent one expands, and that pressure difference pushes heated air toward the edges and draws cooler air inward. In a static test the design looks even, but during walking or reaching, the thermal map becomes patchy, with alternating warm and cool bands that shift with the user's rhythm.
Rethinking Susceptor Geometry as an Active Thermal Control
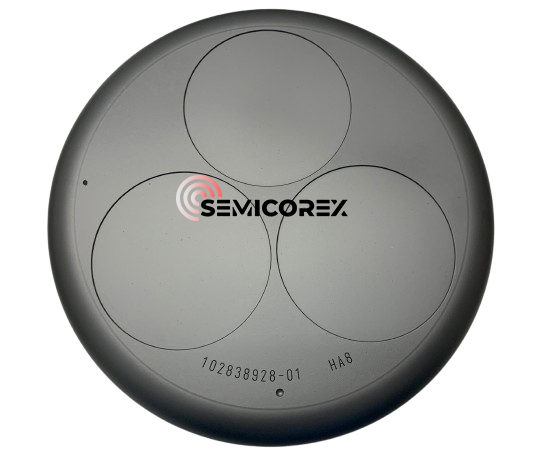
In wafer processing, the susceptor is often treated as a passive supporting plate, yet its shape quietly dictates how heat reaches the wafer. Shallow pockets, tapered rims, and recessed zones create local differences in thermal mass and gas conduction, steering edge-to-center temperature profiles without any external feedback loop.
Rather than relying solely on multi-zone heaters or backside gas pressure, adjusting the susceptor's physical form offers a built-in way to tune heat delivery. A slightly thicker outer ring can hold more thermal energy and reduce edge cooling, while a contoured underside changes how radiant energy is absorbed and re-emitted.
This shift in thinking turns the susceptor into an active design variable. By iterating on pocket depth, rim width, and surface curvature, process engineers can flatten temperature gradients, improve film uniformity, and extend the operating window before external controls even come into play.
How the Custom Profile Keeps Wafer Edges from Underheating
Wafer edges lose heat faster than the center because they have more exposed surface area relative to their volume and sit closer to cooler chamber components. A custom thermal profile compensates by increasing heat delivery specifically near the edge ring or outer zone, which offsets that faster radiative and convective loss.
Instead of applying a uniform setpoint across the whole platen, the custom profile splits the heating surface into zones or uses a tailored power curve that ramps slightly higher toward the periphery. This keeps the edge from lagging behind the center during ramp-up and steady state, without pushing the middle into an overshoot condition.
The result is a flatter temperature distribution across the wafer, which reduces thermal stress and improves thickness uniformity in deposited or annealed layers. Engineers can fine-tune the profile for different wafer sizes and materials, so the edge never becomes a cold spot that triggers defects or non-uniform film growth.
Balancing Gas Flow and Heat Transfer Without Sacrificing Throughput
In many thermal processing tools, pushing more gas through the chamber improves convective heat transfer but also shortens residence time, which can leave the wafer or substrate with uneven temperature distribution. The real challenge is not simply increasing flow or heating power, but shaping the flow path so that the gas picks up heat quickly and delivers it uniformly without creating pressure drops that force longer pump-down or purge steps. Adjusting baffle placement, inlet nozzle geometry, and exhaust port locations often yields a more effective thermal exchange than simply cranking up the gas flow rate.
One practical approach is to use a staged or distributed injection scheme, where a portion of the gas enters near the heated zone to gain thermal energy before mixing with cooler incoming gas downstream. This lets the system maintain a high overall throughput while avoiding cold spots caused by direct impingement of unheated gas on the workpiece. Similarly, tuning the exhaust pressure to keep the gas velocity in a narrow band prevents both stagnation and excessive turbulence, both of which can degrade heat transfer efficiency and slow down the process.
The payoff shows up in batch furnaces and single-wafer rapid thermal processors alike: by carefully matching gas flow dynamics with heater response, operators can run higher wafer counts per hour without sacrificing temperature uniformity or repeatability. Small changes, such as resizing a distribution plate or shifting the exhaust port by a few millimeters, can deliver measurable gains in throughput because the system spends less time recovering from thermal gradients. This integrated view of flow and heat transfer turns what is often seen as a trade-off into a controllable design parameter.
What Changed First: Layer Thickness, Doping, or Defect Density
Time-resolved measurements on operating devices rarely show a single parameter shifting in isolation. In many halide perovskite and organic semiconductor films, the earliest detectable change is a subtle redistribution of thickness—often localized at grain boundaries or near interfaces—before any measurable drift in dopant concentration. This can appear as surface roughening or a slight thinning of the active layer under bias or thermal stress, and it tends to precede changes that show up in electrical characterization.
Dopant migration typically follows the initial geometric perturbation. Once the film has relaxed mechanically or begun to lose material at high-energy sites, mobile ions or molecular dopants start to move along the newly created pathways. Defect density, on the other hand, often lags behind both. It builds up as a consequence of the combined thickness and doping shifts: vacancies left by escaping ions, broken bonds at step edges, and accumulated strain all contribute to a rising background of trap states. This sequence—thickness first, then doping, then defect density—has been observed in several in situ grazing-incidence X-ray and impedance spectroscopy studies.
The exact order can flip depending on the driving force. Under intense illumination with minimal thermal load, defect generation may outpace measurable thickness loss because photochemical reactions create traps directly at the surface. Meanwhile, in systems with a high concentration of volatile dopants, dopant loss can be the first signature of degradation, with thickness changes appearing only after the lattice collapses. Recognizing which parameter moves first is not an academic detail; it determines whether mitigation should target encapsulation, dopant chemistry, or interface passivation.
Production-Scale Metrics That Justify the Design Swap
When a design swap moves from prototype to production, the only numbers that matter are the ones tied to real user impact and operational load. A faster first paint or a smaller JavaScript bundle rarely tells the whole story; what you need are metrics like time-to-interactive under typical device constraints, server CPU per request, and the 95th percentile response time before and after the switch. If the new design can't hold its own on those without extra caching tricks, the swap isn't justified.
Infrastructure cost often becomes the quiet decision-maker. A visually impressive rewrite that doubles database round-trips or forces you to spin up additional instances will erase any front-end gains. Tracking memory residency per worker, connection pool saturation, and cold-start times in your test environment gives you a clearer picture of what the new design actually costs once traffic spikes. The old design may have looked dated, but if it idles at a fraction of the resources, that's a metric worth defending.
Beyond raw performance, the swap should show up in release-level indicators: lower abandonment on key flows, fewer client-side errors, and shorter session recovery after a failure. Those outcomes don't come from synthetic benchmarks alone. Running a canary with a small percentage of real traffic for a week, then comparing crash-free sessions and task completion rates, tells you whether the new design earns its place or just looks better in a slide deck.
FAQ
Pocket depth adjustments, back-side profiling, and selective thinning under the wafer edge help counteract heat loss at the rim. Using a graphite base with a tailored SiC coating thickness can also smooth thermal gradients. These tweaks keep the wafer in a tighter temperature window during growth.
Yield climbs when thickness and composition stay consistent across each wafer. A custom pocket shape reduces slip lines and edge defects, while improved thermal contact lowers the chance of premature nucleation. Fewer rejected wafers per run comes from that repeatability.
Graphite offers excellent thermal conductivity and machinability, but it needs a dense SiC coating to resist chemical attack from precursors. A high-quality coating keeps emissivity stable run after run, so the heat profile doesn't shift as the susceptor ages. That stability is what preserves uniform growth over hundreds of cycles.
The pocket wall height and floor curvature control how gas flows near the wafer edge. A slightly recessed edge or a stepped floor can compensate for faster edge cooling and higher growth rates there. Fine-tuning that geometry makes the boundary layer more uniform, so thickness spread tightens.
Start with thermal imaging and pyrometry scans to map temperature across an empty susceptor. Then run short calibration growths with thin epilayers and measure thickness and doping uniformity. Compare those maps against the previous design before committing to full device stacks.
Standard designs often show a hot edge or a cold center after a few hundred runs, leading to wavelength drift in LEDs or breakdown voltage shifts in power devices. Non-uniform coating wear also creates particles. Custom designs address the exact reactor geometry and gas flow pattern of a given tool.
Particles often come from coating delamination or thermal stress cracking at sharp corners. Smooth transitions, matched thermal expansion between graphite and SiC, and avoiding thin coating edges all reduce flaking. A custom design can also minimize dead zones where gas-phase nucleation deposits loosely.
Look at within-wafer thickness uniformity (typically 1-sigma), sheet resistance mapping, photoluminescence wavelength spread, and surface defect counts. Also track susceptor lifetime and cleaning cycle intervals. Improvement in those numbers shows the design is working, not just the marketing.
Conclusion
Standard pocket designs tend to lose thermal uniformity at the wafer periphery, where the increased surface-to-volume ratio pulls heat away faster than the surrounding susceptor can compensate. Rather than accepting edge underheating as an unavoidable process margin, the custom susceptor treats its own geometry as an active thermal control element. The profile redistributes local thermal mass and adjusts pocket depth near the rim, so the wafer edge sees a hotter, more stable boundary condition. This directly addresses the root cause of non-uniform temperature profiles without requiring higher heater power or slower ramp rates.
The resulting change shows up first in layer thickness distribution, then in doping consistency and defect density across the wafer. Because the custom profile also reshapes the gas flow path near the pocket edge, it maintains efficient precursor delivery while the thermal improvements take hold. Production-scale comparisons confirm the swap is justified: within-wafer thickness variation falls to levels that previously demanded extensive tool tuning, and overall epitaxy yield improves enough to offset the cost of the custom hardware. The edge no longer acts as a yield-limiting zone, and the process window widens for both high-throughput and high-uniformity operation.
Contact Us
Contact Person: Svenja Wei
Email: [email protected]
Tel/WhatsApp: +8613567891907
Website: https://www.semicorex.com