Custom Precision Metal Brackets Designed for Reliable Structural Support
2026-11-16
Structural failure often starts where you least expect it—a bracket that bends under weight, a joint that slowly loosens with vibration. Custom precision metal brackets from BOSI are engineered to remove that uncertainty, delivering dependable support for demanding applications. In this guide, we explore how tailored geometry, material selection, and tight tolerances combine to keep your assembly solid long after installation.
Built Around the Load, Not Around a Catalog
The starting point is never a model number. It is the physical thing sitting on the floor or truck bed. How the weight sits, where the forks have to enter, how high it has to rise, and what clearance remains at the top of the lift all shape the machine. Working from that picture changes the conversation from picking something close enough to matching the task directly.
That means a mast height, fork profile, and counterweight can end up looking wrong in a standard comparison sheet but feeling exactly right on the job. Instead of forcing a load into a predefined envelope, the equipment gets shaped around damage-prone corners, uneven floors, and tight staging areas.
Operators usually notice the difference within the first few cycles. There is less repositioning, fewer last-second adjustments, and a more predictable feel when the weight shifts. The lift becomes an extension of how the work already happens, not a new procedure imposed on the crew.
Tolerances That Don’t Drift After Welding
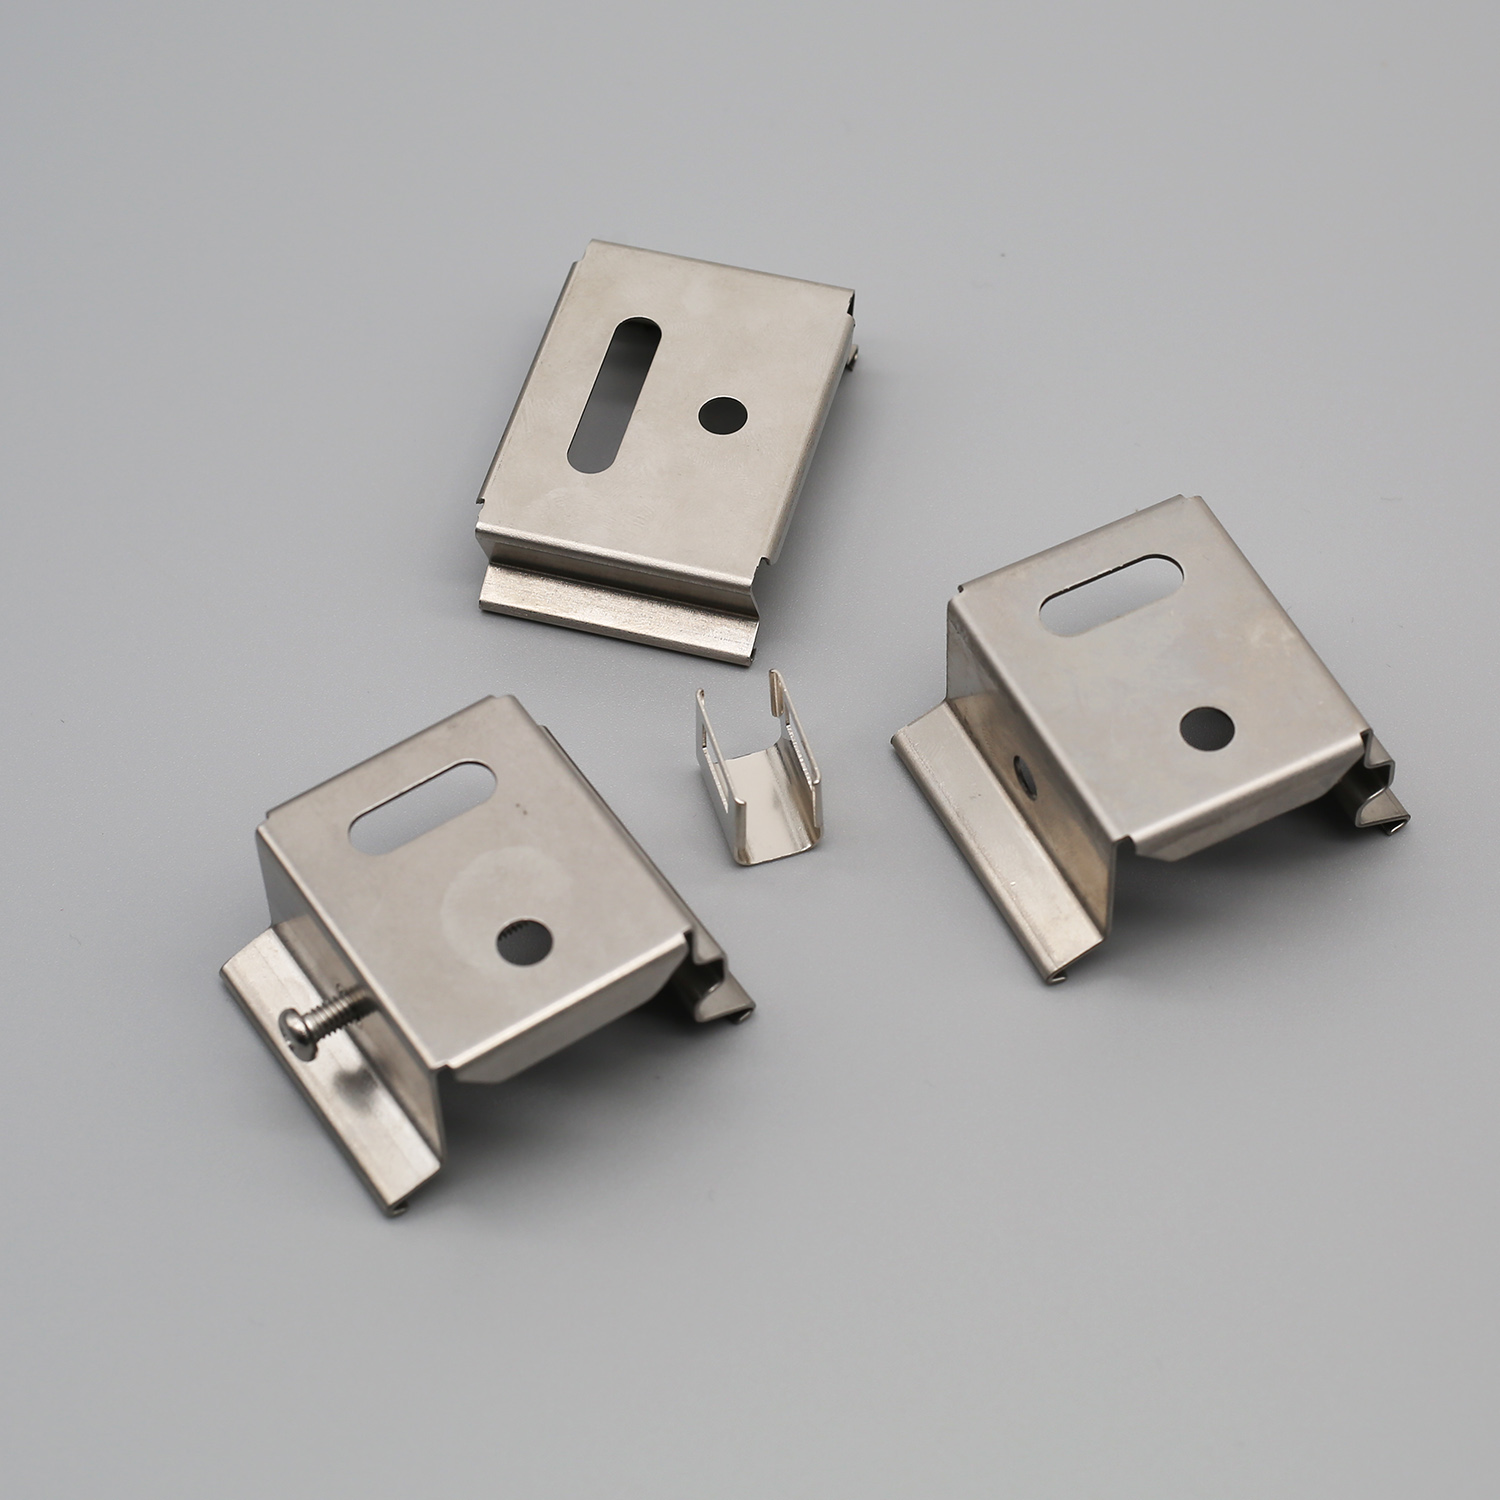
Dimensional stability starts long before the first arc is struck. On these assemblies, critical bores and mating faces are positioned with deliberate restraint, using tack sequences that pull heat away from high-tolerance zones rather than letting it soak in. The result is a welded structure that settles into its final shape almost immediately, without the slow creep that usually follows cooling.
Post-weld checking is not treated as a salvage step here. A short conditioning cycle brings the part to a uniform temperature, then measurements are taken against the machined datums that were locked in before welding. Any movement is recorded, but the intent is not to correct it after the fact. It is to prove that the original setup already accounted for the shrinkage path.
The practical payoff shows up in assembly. Bearings press into place without reaming, bolt patterns line up without forcing, and interchangeable fixtures drop in cleanly. That kind of repeatability does not come from relying on a single tight tolerance on the print; it comes from controlling where the heat goes, how the part is held, and when it is measured.
Choosing Alloys for Corrosion and Fatigue, Not Just Strength
Engineers often default to the highest tensile strength alloy on the datasheet, assuming a bigger number means a safer part. In corrosive or cyclically loaded environments, that assumption falls apart quickly. A precipitation-hardened stainless steel might boast impressive ultimate strength on paper, yet suffer pitting or stress corrosion cracking long before it reaches that limit in service. The smart selection process begins by asking how the material will actually fail, not just how much static load it can carry once.
Fatigue resistance depends heavily on surface condition, residual stress, and microstructural cleanliness. High-strength alloys tend to be more notch-sensitive, meaning a small machining mark or corrosion pit can slash the fatigue life. Switching to a slightly lower-strength grade with better inherent toughness or a more homogeneous grain structure often extends component life in ways a tensile test never reveals. Likewise, corrosion allowances are not just about thickness; they involve choosing an alloy whose passive film reforms quickly after damage, especially in chloride-rich or acidic service conditions.
A practical approach is to shortlist materials by environmental compatibility first, then refine by fatigue endurance at the expected stress amplitude. Duplex stainless steels, for example, offer a useful balance of corrosion resistance and fatigue strength without the extreme notch sensitivity of some martensitic grades. Field failures repeatedly show that a moderate-strength alloy selected for the actual corrosion mechanism and loading spectrum outperforms a stronger alloy picked solely from a specification table.
How Small Geometry Changes Affect Overall Stability
A tiny shift in a gusset plate angle or a few millimeters added to a flange width can look harmless on a drawing, but it alters where forces choose to travel. Stability is not only about material strength; it is heavily shaped by the paths that compression and bending take through a structure. When geometry changes even slightly, those paths reroute, sometimes concentrating stress in a joint that was originally meant to stay lightly loaded.
The effect becomes more pronounced in slender elements and thin-walled sections. A small reduction in a web height or a slight increase in an unsupported length lowers the buckling load more than a linear estimate would suggest. Sudden shifts in stiffness between adjacent regions can also create local hinges, and once a hinge forms, the overall system may reach its critical state well before the material yields.
In practice, this means tolerances and fabrication choices deserve the same attention as the main member sizes. Small edge distances, weld profiles, or cutout radii are not just finishing details; they can control whether a structure drifts into an unstable mode under service load. A few targeted sensitivity checks at the design stage are often enough to reveal which dimensions can move freely and which ones are quietly holding the system together.
Details That Speed Up Installation Without Loosening Fit
Most installation slowdowns come from parts that fight back at the wrong moment—initial threads catch, alignment pins jam, or a clip refuses to seat until you push harder than feels safe. The fix is rarely more force. Small relief angles near the leading edge let mating surfaces glide into position before the locking surfaces make contact. A shallow tapered mouth, for example, centers the part within the first two or three millimeters of travel, so the rest of the stroke follows a clean path instead of relying on the installer to correct angle drift by hand.
Clearance should be uneven, not uniform. Designing a few tenths of a millimeter of extra room only where the part first enters keeps assembly quick without sacrificing the final press or snap. Once the component passes that short entry zone, the original interference returns and holds the fit exactly as intended. Split-ring retainers and stepped collars use the same principle: the flexible section deflects during the fast part of insertion, then relaxes into a groove or shoulder that prevents movement in service. Nothing is loose, but nothing needs to be forced through a long, tight bore.
The biggest time savings often come from details that are invisible on a finished product. A radius instead of a sharp corner at the base of a boss can halve the wiggle time spent finding the start of a hole. Small flats on a round shank give the part a natural orientation, so installers stop flipping it back and forth. When these details are tuned together, the part drops into place with a short, confident push and remains stable under load because the locking geometry still engages fully after the entry aids have done their job.
When Off-the-Shelf Brackets Leave Too Much Movement
Most universal brackets are stamped to fit a range of mounting patterns, and that extra slot length is exactly where the slop begins. Under load, a few thousandths of an inch at the bolt hole turns into visible deflection at the far end of the arm. Once the fastener shifts, it tends to stay shifted, so every vibration cycle works the gap a little wider until alignment drifts and torque settings no longer mean much.
The problem gets worse when the bracket is asked to brace anything that cycles or reverses direction. A bracket that feels solid on the bench can flex enough during use to let a bracket-mounted sensor, guide, or linkage walk off its intended path. The movement rarely shows up as a clean, repeatable offset; it appears as intermittent drift, uneven wear, and fasteners that keep loosening no matter how often they are re-tightened.
Fixing it usually starts with measuring the actual displacement under working load, not just checking the bolt torque. In many cases, a thicker gusset, a tighter tolerance on the mounting holes, or a rigid alignment dowel does more than switching to a larger bolt. The goal is to remove the room for movement before it becomes a wear pattern, because once the bracket has wallowed out its own clearance, replacement is often the only real cure.
FAQ
Most parts stay within ±0.005 in without much trouble. Tighter tolerances are possible, but they depend on the features and material.
A rough sketch works fine. We turn it into a detailed model, confirm the dimensions, and check the bend reliefs before anything gets cut.
6061 aluminum keeps weight down, 304 stainless handles moisture and washdowns, and mild steel often makes sense when cost is the main driver.
We look for sharp corners, thin sections, and stress risers early in the design. Small changes to radii or rib placement can add a lot of fatigue life.
Yes, prototypes are encouraged. Testing a few pieces before a full run tends to save time and avoids producing a batch that needs rework.
Zinc plating, powder coating, anodizing, and passivation are all on the table. The best choice depends on whether the part sits indoors, outdoors, or in a washdown area.
Simple laser-cut parts can ship within a few days. Parts that need forming, welding, or finishing usually land closer to one or two weeks.
Material, quantity, finish, and a drawing or photo with rough dimensions are enough to start. Knowing how the bracket is loaded also helps us suggest the right thickness.
Conclusion
A reliable structural bracket starts with the actual load path rather than a standard catalog shape. Our design process maps how force enters the part, where it concentrates, and how vibration or thermal cycling might work against the connection over time. Because welded assemblies tend to move once heat is introduced, we sequence welds, control heat input, and leave finish machining for the final step so hole positions and mating surfaces do not drift. Alloy selection is handled in the same way: strength alone is rarely the limiting factor, so choices are balanced against corrosion exposure, fatigue life, and how the material behaves after forming or welding. Small geometric details such as a relocated stiffener, a revised bend radius, or added edge distance around a bolt hole often contribute more to long-term stability than a thicker plate would.
The advantage becomes clearest when an off-the-shelf bracket leaves slop in a bolted joint or requires field modifications to fit. Slight clearance in a catalog part can allow movement that shows up as noise, wear, or loosening under repeated loading. Custom brackets close that gap by matching hole tolerances, fastener hardware, and mounting surfaces to the specific structure. Details like slotted holes placed only where needed, chamfered edges that guide bolts into position, and clean access for a torque wrench reduce installation time without weakening the connection. The result is a bracket that assembles predictably, holds its position, and keeps the surrounding structure stable instead of simply filling a space.
Contact Us
Contact Person: Kristy Wu
Email: [email protected]
Tel/WhatsApp: 8613826954049
Website: https://www.dgbosi.com/