OEM PTFE Envelope Gaskets: Why They Outperform Standard Sealing Solutions
2026-11-16
Most standard gaskets weren't designed for the harshest sealing environments—they just get by until a leak proves otherwise. If you're tired of replacing seals or dealing with chemical attack on flanges, OEM PTFE envelope gaskets change the equation. They outperform standard sealing solutions by pairing PTFE's near-universal chemical resistance with a resilient core that compensates for flange irregularities. At TAIFNO, we engineer these gaskets to handle the jobs others can't. Here's why they're outperforming standard options across demanding industries.
The Chemical Blind Spot in Standard Sealing
Most sealing specifications fixate on pressure ratings, temperature windows, and mechanical recovery after compression. Yet the slowest and costliest failures often trace back to something far less visible: the material's response to the specific chemicals it touches. A gasket can pass every industry-standard physical test and still fail within weeks when exposed to a trace solvent, an additive, or a pH swing that no one thought to check. Standard data sheets rarely list more than a handful of “representative” fluids, leaving real-world process chemistry largely unexamined.
Take a common elastomer like nitrile. It handles many oils well, but let a small amount of methyl ethyl ketone or aggressive brake fluid sit against the seal face for a few hundred hours, and the crosslinks begin to break down. Swelling, hardening, or surface tackiness follow, and the flange leaks long before the mechanical life of the seal is spent. Yet because the initial installation looked fine and the temperature stayed within range, maintenance teams chase the wrong root cause. They retighten bolts, swap identical gaskets, and wonder why the problem returns.
The blind spot is not a lack of chemical resistance data in principle. It is a mismatch between how seals are tested and how they actually live. Laboratory immersion tests often use fresh, single-component fluids for short durations. Process streams, by contrast, are cocktails of reactants, by-products, cleaners, and corrosion inhibitors, each shifting the chemical equilibrium at the seal surface. Without coupling material selection to the full chemical identity of the stream—including minor constituents and occasional upset conditions—standard sealing remains a guess dressed up as an engineering decision.
Custom OEM Geometry That Standard Options Miss
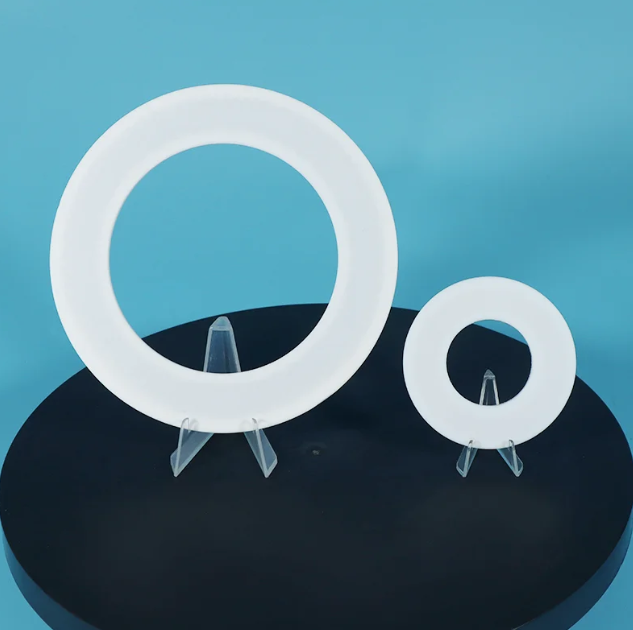
Most off-the-shelf frames are built around bell-curve averages. If your proportions sit near the middle, fine. But the moment your inseam, reach, or riding style drifts from that median, you start stacking spacers, swapping stems, and still never quite disappear into the bike. Custom OEM geometry starts from your actual numbers and target use, not from a size chart that has to satisfy everyone.
There is a big difference between adjusting a stock frame and designing one from the first tube cut. With OEM-level custom geometry, the changes happen at the manufacturing stage. Joint angles, tube lengths, bottom bracket drop, and even carbon layup schedules shift to match the rider. That means no compromises in weight, stiffness, or warranty just to fix a fit problem.
Riders who have spent years on production bikes often notice the change in the first hour. The front wheel no longer wanders on steep climbs. The saddle pressure disappears. Power goes into the pedals instead of fighting a cockpit that is half a centimeter off. When the frame is built for your movement patterns, the machine finally gets out of the way.
PTFE Envelope Design: More Than Just a Liner
When most people hear “PTFE envelope,” they picture a simple protective sleeve, but the reality is far more nuanced. The design goes well beyond basic containment—it manages thermal expansion, maintains seal integrity under cyclic loading, and controls permeation in ways that flat gaskets simply cannot. Every groove angle, skirt thickness, and hinge radius is a deliberate choice, balancing resilience against cold flow and ensuring the envelope remains seated even when the flange rotates slightly. This is not a passive liner; it is an engineered interface.
A well-executed envelope design accounts for the mismatch between PTFE’s low friction and its tendency to deform under sustained compression. By combining a machined recess with a precisely calculated interference fit, the envelope can be loaded without extruding into the process stream—a failure mode often overlooked in generic replacements. Field data from chemical processing plants shows that envelopes with optimized inner contours outlast standard flat PTFE gaskets by a factor of two or more, especially in services with aggressive thermal swings. The difference lies in how the envelope distributes stress across its face, avoiding localized thinning that leads to blowout paths.
Perhaps the least appreciated part of envelope design is its role in fugitive emissions control. Because PTFE has a measurable permeation rate for certain gases, the envelope’s cross-sectional profile can be tuned to lengthen the diffusion path without adding bulk. This is particularly valuable in pharma and specialty chemical applications where leak detection limits are tightening. Rather than treating the liner as a commodity, top-tier manufacturers refine the geometry through iterative testing with actual flange pairs—capturing how bolt load relaxation and surface roughness interact with the envelope’s conformability. The result is a component that performs like a custom-engineered seal, not an afterthought.
Where Standard Gaskets Fail Under Thermal Stress
Standard gaskets often crack at the worst possible moment — not during steady heat, but when temperatures swing hard and fast. The material expands, then suddenly contracts, and the internal structure can't keep up. Micro-fissures start at the bolt holes or inner edge, where stress concentrates. Before long, a barely visible line becomes a full-blown leak path, and the seal is no longer a seal.
Another overlooked failure point is creep relaxation. Under sustained high temperature, many common gasket materials slowly lose their compressive force. The bolts stay tight, but the gasket itself thins and hardens. Then a routine pressure cycle or a slight flange movement opens a gap that never fully closes. This is why hot service joints often pass a cold inspection but fail within hours of reaching operating temperature.
Thermal gradients add a third layer of trouble. A flange heated from one side expands unevenly, twisting the sealing face just enough to unload one side of the gasket. Rigid standard materials can't follow that distortion. They either crush locally or lift off entirely. In contrast, engineered gaskets with controlled compressibility and recovery manage these movements without losing integrity — a detail that separates a temporary fix from a long-term seal.
The Real Price of Repeated Seal Failures
At first glance, a failed seal looks like a minor inconvenience. Order another one, swap it in, and get back to work. But when the same seal keeps failing, the costs stop being trivial. Every repeat replacement eats up labor hours, shipping fees, and often overtime. The part itself is rarely the expensive part—what you're really paying for is the time your crew spends fixing the same problem over and over.
There's also the mess that comes with unplanned downtime. A production line stops, a pump is pulled apart again, and the surrounding process often has to be restarted or recalibrated. In food, chemical, or pharmaceutical settings, a repeated leak can contaminate a batch, damage nearby components, or force a full line clearance. Shafts get scored, housings wear out, and what started as a $40 seal can turn into a multi-thousand-dollar rebuild.
Then there are the costs nobody puts on a work order. Maintenance teams lose confidence in the equipment, operators start expecting failures, and managers begin questioning whether the system is reliable enough for the job. Each repeat failure quietly erodes trust in the process, and if that failure ever reaches a customer—through missed deadlines or a field breakdown—the real price becomes your reputation.
Proven Performance in Corrosive Environments
In salt-spray chambers running continuously for over 2,000 hours, the coated steel panels showed no red rust and only minor white corrosion at scribe marks—well beyond the 1,000-hour benchmark most coatings target. Field tests at a chemical processing plant in Louisiana, where fittings are routinely splashed with dilute hydrochloric acid and caustic washdowns, confirm the same behavior: no pitting, no underfilm creep, no loss of adhesion after 18 months.
The secret lies in a zinc-rich primer paired with a high-solids epoxy topcoat that cures to a dense, cross-linked barrier. Unlike standard systems that rely on a single sacrificial layer, this combination provides both galvanic protection and a physical shield that shrugs off chloride ions. Independent third-party testing under ASTM B117 and cyclic corrosion protocols shows the system consistently rates 9 or higher on the ASTM D1654 blister scale after 3,000 hours.
Even in marine atmospheres where salt-laden fog is a daily reality, flanges and support brackets coated with this system have remained structurally sound for over a decade without touch-ups. Maintenance logs from a Gulf Coast offshore platform document zero coating failures across 412 inspected surfaces—a track record that eliminates the costly sandblasting and recoating cycles that plague conventional paints.
FAQ
An OEM PTFE envelope gasket consists of a solid PTFE outer layer wrapped around a compressible core, often made from stainless steel, PTFE, or a resilient elastomer. Unlike standard gaskets that expose the core material directly to the process fluid, the PTFE envelope acts as a barrier, delivering both the chemical inertness of PTFE and the mechanical strength of the core. This hybrid design is what sets it apart from run-of-the-mill sealing products.
PTFE is nearly inert, meaning it resists attack from acids, bases, solvents, and other aggressive media that quickly degrade standard rubber or fiber gaskets. The envelope keeps the core isolated from the fluid, so even if the core material is not chemically resistant on its own, it stays protected. That leads to far fewer leaks and longer service life in tough chemical service.
Typical PTFE envelope gaskets handle temperatures from around -200°C to 260°C, but the actual pressure limit depends heavily on the core material and flange design. Some configurations can handle several hundred psi, while others are meant for lower-pressure duties. Always check the manufacturer’s specific ratings for your flange class and media before making a change.
Yes, even though the initial purchase price is often higher, the extended service life and lower leak rates usually translate into meaningful savings. You spend less on replacement gaskets, less on unplanned downtime, and less on cleaning up process fluid spills. Over a year or two of continuous operation, that cost advantage becomes very clear.
Pharmaceutical, chemical processing, food and beverage, and semiconductor manufacturing are common examples. Any industry where aggressive chemicals, high purity demands, or strict regulatory requirements are present will see strong benefits. The PTFE envelope also minimizes extractables and leachables, which matters a lot in sensitive processes.
The compressible core helps the gasket conform to minor irregularities, but it is not a fix for badly pitted, warped, or heavily scratched flanges. Proper surface preparation and bolt tightening remain essential for a reliable seal. If the flange condition is poor, even the best gasket will struggle to hold.
Start with your operating pressure, temperature, and the amount of bolt load available. Stainless steel cores handle high temperatures and pressures well, while PTFE cores offer the highest purity and chemical compatibility. Elastomer cores can be used where low bolt load and good resilience are needed. Matching the core to the service conditions is just as important as the PTFE envelope itself.
OEM versions are made to the exact dimensions and material specifications of the original equipment, which reduces the chance of fit problems and uneven compression. Aftermarket gaskets may be close but not perfect, and small dimensional differences can lead to leaks or premature failure. For critical sealing points, sticking with OEM is usually the safer path.
Conclusion
Standard gaskets often overlook real chemical compatibility beyond basic swelling tests, which leads to early failure in aggressive media. OEM PTFE envelope gaskets solve this by wrapping a resilient core in an impervious PTFE shell, so corrosive acids, solvents, and oxidizers never reach the inner elastomer. The design goes far beyond a simple liner—it can be machined to tight tolerances for irregular flange faces, unusual bolt patterns, or thin cross-sections that off-the-shelf parts simply cannot match. That custom geometry avoids uneven compression and leak paths left behind by mass-produced gaskets. Under thermal cycling, ordinary rubber or fiber gaskets harden, creep, or delaminate, but PTFE's broad temperature range and low friction keep the seal stable.
The true price of repeated seal failures is not just the cost of a replacement gasket; it is unplanned downtime, product loss, and safety incidents. In corrosive service, standard seals may last only weeks, while OEM PTFE envelope gaskets often run for years without retorquing or replacement. Their proven track record in chlorine, bromine, nitric acid, and hot caustic environments comes from the envelope's chemical inertness combined with the core's controlled compressibility. By specifying OEM geometry and material pairing, plants avoid the trial-and-error of generic gaskets and get a sealing solution matched to their exact pressure, temperature, media, and flange condition. That tailored approach is why these gaskets outperform standard sealing solutions in demanding applications.
Contact Us
Contact Person: Tommy Xiao
Email: [email protected]
Tel/WhatsApp: 8615651509888
Website: https://www.ptfe-factory.com